
How Much Do Machined Metal Parts Cost in 2026? A Buyer's Cost Model
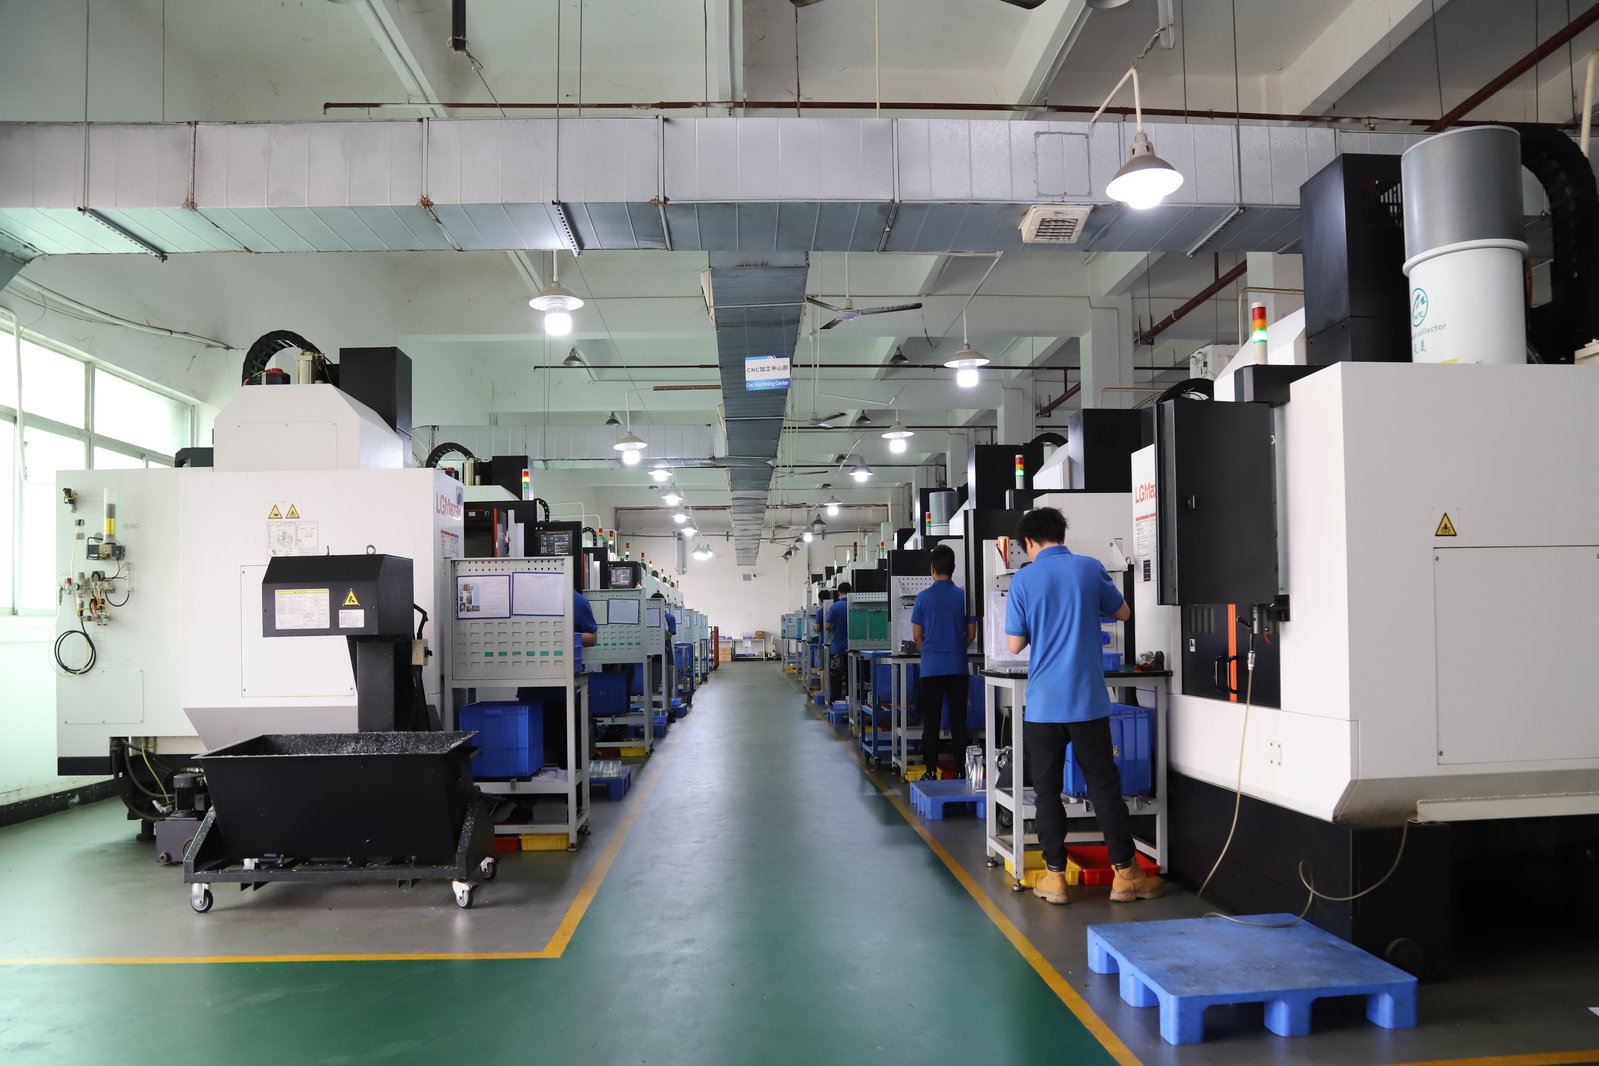
The price of a machined metal part and the date it ships come from the same place: the process steps on its route. A simple bracket that needs a few operations is fast and economical; the same part with milled features, a ground seat, a finish, and a second process is slow and expensive, not because it is bigger, but because every step is a setup, a tool, an inspection point, and a day on the calendar. Buyers who separate the cost conversation from the delivery-date conversation are pricing half the problem, because the schedule is a cost lever in its own right: a part that ships on time keeps your line moving, and a date that slips is a cost that never appears on any invoice. This guide is the buyer's cost model for machined metal parts in 2026 — the line items inside a quote, why cost and lead time share one map, how material, tolerance, finish, and quantity move each line, and how to build a budget that prices the part and the schedule together.
What does a machined metal parts quote actually pay for?
Strip any serious quote for machined metal parts back to its bones and the same lines appear underneath the formatting. Each line has a job, and each line can hide a cost if the supplier does not name it.
| Line item | What it pays for | What moves it |
|---|---|---|
| Material | The bar, plate, or block at the grade on the drawing | Grade, form, and whether the lot is verified against a mill certificate |
| Setup and programming | Fixturing, toolpath work, and first-piece prove-out | A fixed cost per order that dominates low-volume work |
| Machining time | Spindle minutes to cut the features and hold the tolerances | Feature count, material toughness, and tolerance per feature |
| Secondary operations | Threading, anodizing, plating, heat treatment, and similar steps | Each step adds a line and a day; the hand-off is part of the price |
| Grinding | The features a mill or lathe cannot hold | A separate process family with its own machine and measurement |
| Inspection and documentation | CMM time, SPC records, material certificates, reports | Every tight characteristic adds measurement time and proof |
There is no honest single number for a machined metal part, because the drawing, the material, the quantity, and the process route decide it together. What stays consistent is the structure, and the structure is what makes the quote readable and the date believable.
Why do cost and lead time share the same map?
The hub of this site is lead time and capacity, and the cost model runs on the same rails. Lead times here are set in roughly three tiers — about 3 days for simple parts, 7 days for standard work, and up to 30 days for complex parts with many process steps or finishing — and the price climbs the same ladder. A part that lands in the fast tier is fast because it is simple: few steps, one material, no finishing queue. A part in the long tier is slow because it is complex: more setups, more processes, more inspection, and sometimes a surface finish that pushes it past the machine floor entirely.
Read the two quotes — the money and the date — as one document. When a supplier prices a part and dates a different process route than the one it priced, the schedule is hiding a cost that will surface as an expediting charge, a late shipment, or a line stoppage. The honest quote states one route, and the price and the lead time both come from it. A buyer who checks that the two match is reading the cost model correctly.
How does the machine mix set the price and the date?
A supplier's capacity is the other half of its cost structure. The floor behind this site runs 100+ production machines — 3-axis (50+), 4-axis (20+), 5-axis (20+) milling, 25+ lathes, and 7+ grinders — across a 6,800 m² facility, with 100+ employees and 20+ inspection instruments. That mix matters to your quote in two ways.
First, the right machine for the geometry is the economical and the fast machine: a part that needs one setup on a five-axis center or a mill-turn machine is cheaper and quicker than the same part routed across three machines. Second, depth of capacity is price insurance on the schedule. A floor with that mix can absorb a spike without displacing your job, which is what keeps the quoted date — and the cost of missing it — real. The machine list underneath the quote is the first page of both the cost model and the schedule: setups are the hidden cost of a schedule, and the machine mix is what keeps the number of setups honest.
Which material should a machined-parts budget assume?
Material moves a machining quote twice: once as stock, and again at the cutting edge. Aluminum 6061 is the economical default for housings and brackets; the free-machining grades — 303 stainless, 12L14 steel, C360 brass — keep turned and machined parts economical where the application allows them; and the demanding grades — 304 and 316 stainless that work-harden, titanium, and the heat-treatable steels — run slower, wear tools, and stretch both the price and the schedule on every feature that touches them.
Two rules keep the material line honest. First, name the grade on the drawing, not the family, and verify the shop checks incoming stock against its mill certificate — incoming lots on this floor are XRF-checked against the mill certificate before machining, so a substituted alloy is caught at the door rather than discovered in service. Second, read the material as a schedule decision as well as a price decision: a material that moves a part from the 7-day tier into the 30-day tier has changed the cost of the program even if the per-piece number looks the same.
How much do tolerance and surface finish move the price and the schedule?
Tolerance is the steepest part of the machining cost curve, and it stretches the schedule on the same features. A dimension at ±0.05 mm machines in one pass; a feature at ±0.003 mm may need a controlled finishing pass; and a surface at ±0.002 mm needs grinding, a separate process family with its own queue. On this floor, milling and turning hold ±0.003 mm and grinding reaches ±0.002 mm, verified on Hexagon CMMs with process capability demonstrated at Cpk 1.851 against an initial-study target of Ppk ≥ 1.67. Knowing what each process holds lets the planner route the part once, to the process that can hold the tolerance, which is what keeps both the price and the date from carrying a second attempt.
Read the tolerance band before you read the index. Cpk is a ratio of the tolerance band to the process spread, not an absolute measure of accuracy. The figure above was recorded on a length characteristic with a 0.4 mm band (76.1–76.5 mm) — wide by design. Hold the same process spread against a ±0.005 mm feature and it fails outright. Ask for the band, the subgroup count and the sampling window on every capability number a supplier quotes.
Surface finishing follows the same logic. Any surface finish that leaves the machine floor — anodizing, plating, passivation — adds a hand-off and a queue, and the site's rule is blunt: surface finishing pushes a part into the long tier. Specify the finish on the features that earn it, pair it with the tolerance on the same face when you review the drawing, and the part will be priced and dated for the process it actually needs.
How does quantity bend the unit price on machined parts?
The setup is the same whether you order one part or a thousand: the fixture, the program, and the first-piece prove-out cost the same either way. At one piece, that fixed cost lands entirely on the part, which is why a prototype looks expensive. As quantity rises, the setup spreads across the run and the unit price falls toward the sum of the material and the machining time.
Quantity has a schedule dimension too. A prototype runs on a different schedule than a production order — the prototype proves the process at its full setup weight, and the production run follows the same route with the fixed lines amortized. Use the MOQ of 1 piece to validate the part and the process before you commit volume, because the cost of proving one part is trivial next to the cost of a wrong lot. And give the supplier your annual volume and your ramp: a real forecast lets the factory reserve capacity, which is what keeps production lead times from surprising you later. Capacity reservation is a cost decision as much as a scheduling one — it is the difference between a date you can plan on and a date you hope for.
What hidden costs sit inside a machined-parts quote?
The visible lines are half the price; the other half hides in what the quote does not say. A quote that prices per piece but not per part number has hidden the setup you will pay again on the reorder. A quote that absorbs inspection into the margin has hidden the CMM report you will recreate at incoming. A quote that names a tolerance without the process that holds it has hidden the grinding step from the total. A quote that prices a part in one tier and dates it in another has hidden the schedule risk. And a quote from a supplier that cannot show its machine list, its measurement, or its certificate numbers has hidden the verification entirely.
The supplier itself is the largest hidden cost of all, and on a scheduling hub, the trading desk is the schedule risk made flesh. A trading desk resells someone else's capacity, which means it cannot protect your date when the real factory fills up. The brand behind this site is Dongguan Zhuohang Ltd, incorporated in 2005, registration number 91441900MA4UWT6X39, operating the 6,800 m² facility with 100+ machines and 100+ employees described above. Its certificates carry numbers a buyer can verify: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (product design excluded) (131941/A/0001/SM/En), and ISO 14001:2015 (116024/B/0001/UK/En). When the entity, the floor, and the capacity are checkable in writing, the margin stays in the quote and the date stays in the schedule where you can plan on it.
How do you compare two machined parts quotes on the same basis?
A quote you can compare states its assumptions, and on machined parts, the most important assumptions are the route and the date. Make sure every supplier shows the material grade and how the incoming lot is verified, the process route for every feature with the machine type, the tolerance and finish it will actually hold per characteristic, the lead-time tier that route earns, the capacity behind the date, and the quantity tier with prototype and production separated.
Compare the itemized routes at the quantity you actually plan to order, because the same drawing at fifty pieces and at five thousand is two different cost problems — the setup is the same, but its weight per piece is not. And weigh the price against the schedule in the same breath. The lowest quote on machined parts is rarely the lowest total cost: the part that arrives late, or without its CMM report or material certificate, is the part that costs you a line stoppage or an inspection you have to redo. The evidence and the date are part of the product.
How do you build a 2026 machined-parts budget that holds?
Build the budget the way this site plans a schedule — route first, capacity second, quantity third.
- Get the DFM review before you fix the number. Send the drawing and ask the supplier to flag the features that are tighter than the function needs, the features that force a second process, and the finishes that push the part into the long tier. Fix the drawing first; then budget the fixed part, not the first draft.
- Ask for the route and the tier in the quote. Which process runs each feature, and which lead-time tier does the route earn? A part priced in one tier and dated in another is a quote that has hidden its real cost. The route, the price, and the date should come from the same page.
- Share your volume and reserve the capacity. Give the supplier your annual volume and your ramp, confirm how the reserved capacity is protected, and quote the prototype and the production tier on the same page. Budget both at your real quantity, and the 2026 number will survive the first invoice, and the first delivery date.
Keep the closing rule in front of you: read the quote as a route with a date, not a total, and the machined-parts budget you build will hold across the drawing changes, quantity shifts, and reorders that real sourcing always brings.
Frequently Asked Questions
How much do machined metal parts cost in 2026?
No honest shop quotes machined parts without a drawing, because the price is set by the material grade, the process route, the tolerance band, the finish, and the quantity. A simple 6061 bracket at production quantity sits low; a complex part with tight tolerance, grinding, and a finish at prototype quantity sits far higher. Budget the route the drawing actually needs, and the date that route earns.
Why does the delivery date matter to the cost?
Because cost and lead time come from the same process route. A part with many steps costs more and takes longer, and a supplier that prices one route and dates another has hidden the schedule risk. Planning on a date that slips is a cost that never appears on an invoice.
What tolerances can you hold?
Milling and turning hold ±0.003 mm on critical features, and precision grinding reaches ±0.002 mm, verified on Hexagon CMMs with process capability demonstrated at Cpk 1.851 against an initial-study target of Ppk ≥ 1.67.
What are the lead times, and can capacity be reserved?
Lead times run roughly 3 / 7 / 30 days, set by complexity and process steps. Share your annual volume and your ramp, and the factory reserves capacity so production lead times do not surprise you later.
What is the minimum order, and do reorders cost less?
The MOQ is 1 piece, so a prototype and a production run can share one route and one machine. Once the process is proven, reorders skip the first-article prove-out and ship faster at a lower per-piece rate, because the setup is already documented.
Which company and certificates back the quote?
The brand behind this site is Dongguan Zhuohang Ltd (registration 91441900MA4UWT6X39), incorporated in 2005, at a 6,800 m² facility with 100+ machines and 100+ employees, certified to ISO 9001:2015, IATF 16949:2016 (product design excluded), and ISO 14001:2015 with verifiable certificate numbers.
Want a quote priced and dated from the same route?
Email the STEP or IGES model, the material grade, and the toleranced 2D drawing to [email protected] or call +86 13126536955. You will get a design-for-manufacturing review, an honest delivery date, and an itemized quote with the prototype and production tiers on the same page.