
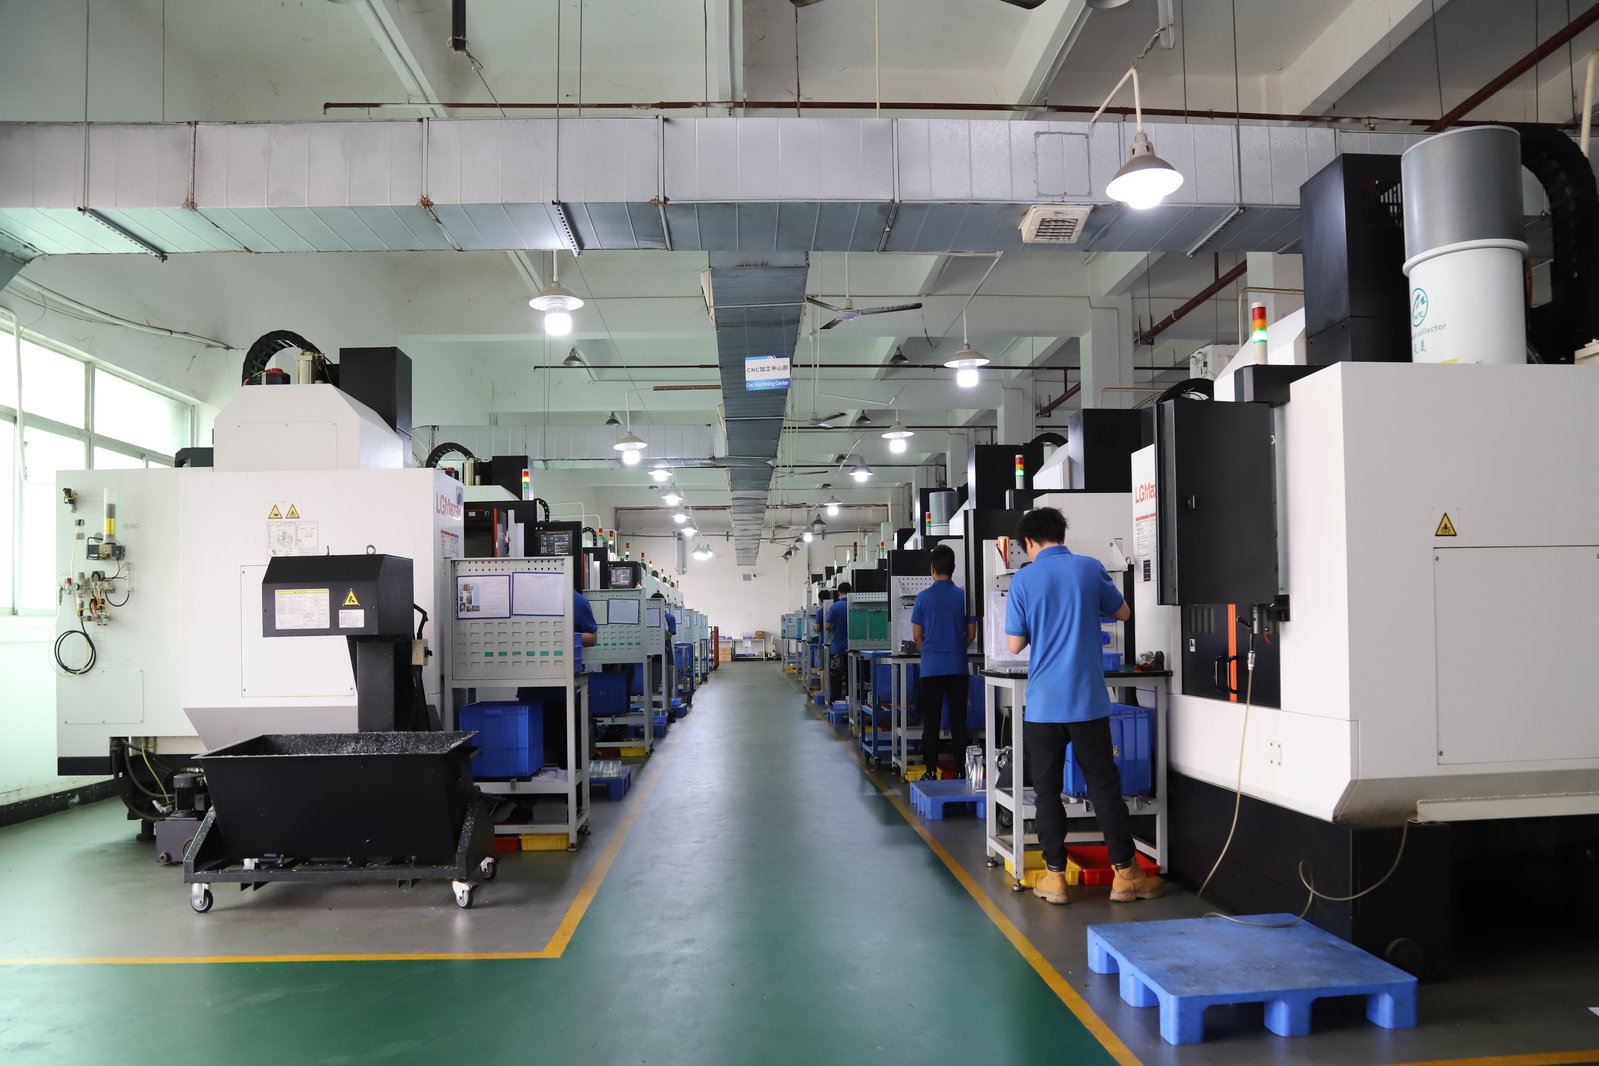
Most buyers think of a machined metal part as coming from a single supplier, and the single supplier thinks of it as coming from several. The bar arrives from a distributor that holds the stock and its certificate; the machining floor cuts it and holds the tolerances; and if the drawing carries a finish, the anodizing, plating or heat treatment may run at a specialist partner. Each of those links is a separate organization with its own risks, and each link's failure looks identical from your dock — the order is late, wrong or unproven. This guide walks the verification of the route link by link, and the payment structure that follows each link's evidence.
Why verify a metal part order as a route rather than as a single purchase?
A route has seams, and seams are where orders fail. The stock link can fail when the distributor delivers a grade that does not match its certificate, or delivers late because the size was not stocked. The machining link can fail when the floor cannot hold the tolerance or cannot schedule the part. The finishing link can fail when the partner's batch runs late, or its process record does not arrive with the parts, or the coating does not match the class the drawing named. Every one of those failures is a failure of the whole order, and none of them is visible when the buyer verifies only the machining floor.
Reading the order as a route changes what the buyer asks at the start. Instead of asking one supplier to be credible, the buyer asks who holds each link and how each link is controlled. The machining floor should name its distributor, its finishers and its heat-treatment partner, and describe what each returns with the lot. A floor that can name its route and its controls is a floor that understands where its orders can fail; one that answers in generalities about quality is a floor that has not looked at its own seams. The route conversation is the first act of the audit, and it decides where the rest of the verification should point.
How do I verify the alloy stock before it becomes my parts?
The stock link is the only one that can be verified before it disappears into the parts, because once a bar is machined the alloy can no longer be seen. The verification starts in the order itself: name the grade, the condition and the form your drawing requires, because the certificate can only confirm what the order specifies. Require the mill certificate with the heat or lot number, and confirm that the machining floor verifies the incoming lot against that certificate before any cutting. The incoming check — an alloy analysis on the physical stock — is the link between the certificate and the metal, and it is the step most often missing when a lot's material story collapses.
The stock link also has a schedule half that belongs in the same conversation. Ask whether the grade and size are stocked by the distributor or must be ordered, because a non-stock size turns the stock link into the longest leg of the route, and a schedule quoted past it is a schedule that hides its own foundation. Where a metal part program repeats, the strongest move is to hold the stock ahead of the machining release, so the stock link drops out of the critical path entirely. A route whose stock is verified, stocked and scheduled is a route whose first link is real; one whose stock is assumed is a route starting on a guess.
How do I verify the machining floor that cuts the parts?
The machining floor is the link where the geometry is made, and it earns the core of the audit: the entity registration checked against the quotation and the payment account, the machine list confirmed on a live walk-through, the certificate numbers resolved with their registrar, and a redacted sample of a past lot's paperwork read for internal consistency. Each of these checks is the same one applied to any machine shop, and together they establish that the floor that will cut your part is the floor it claims to be, running the machines it claims to run, under the quality system it claims to hold.
The floor-specific half of the check is the geometry fit. Ask which machine class will run your part, why that class, and what similar work the floor has shipped recently, because a metal part's difficulty lives in its features rather than in its material family. A floor that has proven it can hold your kind of tolerance story, on your kind of geometry, is demonstrating the capability the order needs; one whose past work is all simpler than yours is asking you to fund its learning curve. The machining floor is where the route's quality is actually produced, and the verification of it is the part of the audit that no other link can substitute for.
The strongest test of the whole route is a pilot lot that exercises every link at once. A small first order that runs the distributor's stock through the floor's machining and, if the drawing carries it, through the finishing partner's line produces the evidence all three links need to be judged on one shipment: the stock certificate arrived with the metal, the first article measured against the drawing, and the finish returned with its process record. The pilot is priced at the size of the risk, and its report is the document that qualifies the route for volume. A buyer who skips the pilot and releases volume against the floor's brochure is paying the qualification cost at volume prices, which is the most expensive way to learn that one of the three links was never really proven.
How do I verify a finishing partner I will never visit?
The finishing link is the one most buyers can never inspect directly, because the anodize line or the plating shop is a specialist elsewhere. The verification therefore runs through the machining floor, and the questions are about control rather than trust. Ask how the floor qualifies its finishers, what records each finisher returns with its lots, and what happens when a finish fails — whether the floor investigates and recovers, or whether the parts simply come back and the argument begins. A floor that treats its finishers as part of its quality system, with qualification records and returned process documentation, is running a controlled route; one that treats them as vendors whose output is taken on faith is running a handoff.
The documentary half of the finishing link belongs in the order. Name the finish by its class and its standard at the RFQ, because a finish named vaguely is a finish the finisher can interpret loosely, and require the finisher's process record to ship with the parts so the treatment can be verified as well as the machining. When the finish is dimensional — anodize or plating grows a layer — state whether the drawing's dimensions are before or after treatment, because that single sentence decides whether the parts fit after coating. A finishing link that is qualified, specified and documented is a link the route can stand on; one that is not is a seam waiting to fail.
The failure modes of the finishing link deserve their own questions, because a failed finish rarely fails alone. Anodize that comes back with the wrong color or a thin coating means the parts return to the finisher, the machining floor waits, and the schedule absorbs the round trip; plating that blisters means the parts may need stripping before they can be re-treated, and stripping can attack the machined surface underneath. Ask the floor what it does when a finish lot fails — whether it has a recovery process, whether the finisher accepts responsibility and re-runs, and who carries the cost of the round trip. A floor with a documented answer to that question is managing its finishing risk; one without an answer is managing it by hoping, which is not a management method at all.
What should the payment structure be when the route has several links?
A route with several links earns its payments link by link, because each tranche can then be released against the evidence of the link that produced it. The deposit covers the stock and the machining commitment, and it is the only money that moves before any work. The middle tranche releases when the first article measures correctly and, if a finish is in the route, when the finished parts return with their process record — the coating, the class, the batch result. The balance releases against the completed documentation and the shipping release, when every link's evidence is in hand and the parts are genuinely ready to move.
The buyer's discipline on a routed order is to define each link's evidence in the purchase order before the deposit, so the middle tranche waits for exactly the documents that prove the route held. A first article that measures correctly but a finish whose record is missing has proven two links of three, and the missing link's evidence should hold the tranche until it arrives. The payment ladder on a routed order is the audit made financial: each rung verifies one link, and the money does not move past a link whose evidence is absent. That is the structure that turns a three-organization route into a single controlled order.
What documentation should a metal part lot carry from all three links?
The shipping package of a routed metal part order is the record of all three links, and it should read as one chain. The stock certificate with its heat opens the chain, the machining floor's first-article and lot reports carry the geometry, and the finisher's process records close it where treatment was used — every document naming the same order so the chain can be read backward from your dock to the distributor's shelf. A lot whose documents do not align across the links is a lot whose route has a seam, and the seam is where the audit failed even if every individual document looks plausible.
Contracting the route closes the same gaps on paper. Put the distributor's requirement into the flow-down of the order — the grade, the condition and the certificate requirement travel from your drawing into the floor's purchase from the distributor, so the stock link is bound by the same specification that binds the machining. Require the floor to name its finishing partners in the quotation and to warrant their work as part of its own, because a buyer who orders a coated part from one supplier should not have to chase a second supplier's quality record later. When the order document binds every link to the same specification and the same evidence, the route stops being three organizations and becomes one contractual chain, which is the only form in which a three-link route can be managed as a single purchase.
The receiving check is where the chain is tested against the physical parts. Confirm the certificate names the heat the report claims, measure a critical feature against the lot report, and verify the finish against its process record before the parts enter your stock. When the parts, the documents and the links all agree, the route has held from bar to box, and the order is what the audit predicted it would be. For how the machining floor manages the links it does not own, the quality page on this site explains the controls, and the services page covers the finishing partners a route can carry. A metal part order verified route by route, with stock, machining and finishing each proven and each documented, is an order whose price buys the whole chain rather than a single link of it.
Frequently Asked Questions
Why verify a metal part order as a route rather than as a single purchase?
Because most metal parts touch more than one organization before they reach you: the distributor with its stock, the machining floor, and possibly a finishing partner. Each link can fail independently, and each link's failure looks like the whole order failing, so the verification has to cover the route.
How do I verify the alloy stock before it becomes my parts?
Name the grade, condition and form in the order, require the mill certificate with the heat number, and confirm the floor verifies the incoming lot against that certificate before cutting. The stock link cannot be checked after machining, so its verification belongs before the first chip.
How do I verify the machining floor that cuts the parts?
With the checks that apply to any machine shop: registration, machine list on a live walk, certificate numbers with their registrar, and a redacted sample lot. Then check the geometry fit, which machine class runs your part and what similar work the floor has shipped.
How do I verify a finishing partner I will never visit?
Ask the machining floor how it qualifies the finisher, what records each finisher returns, and what happens when a finish fails. A floor that treats finishers as part of its quality system is running a route; one that treats them as vendors is running a handoff.
What should the payment structure be when the route has several links?
Release money against evidence from the link that produced it. The deposit covers stock and machining commitment; the middle tranche releases when the first article measures and any finish returns with its process record; the balance releases against the completed documentation and the shipping release.
What documentation should a metal part lot carry from all three links?
The stock certificate with its heat, the machining floor's first-article and lot reports, and the finisher's process records — all naming the same order so the chain reads backward. A lot whose documents do not align across the links is a lot whose route has a seam.
When should the route verification be repeated?
When any link changes: a new distributor, a different finishing partner, a new material family, or a process moved in-house. A route that was verified once is a claim until it is verified again, and a change in any link invalidates the part of the verification that covered the old link.
Want a metal part order quoted with every link of the route named?
Email the STEP or IGES model with your toleranced drawing to [email protected] or call +86 13126536955, and receive the stock plan, the machining plan and the finishing record structure for your part.